Pages

Showing posts with label high pressure. Show all posts

Sunday, 15 November 2015

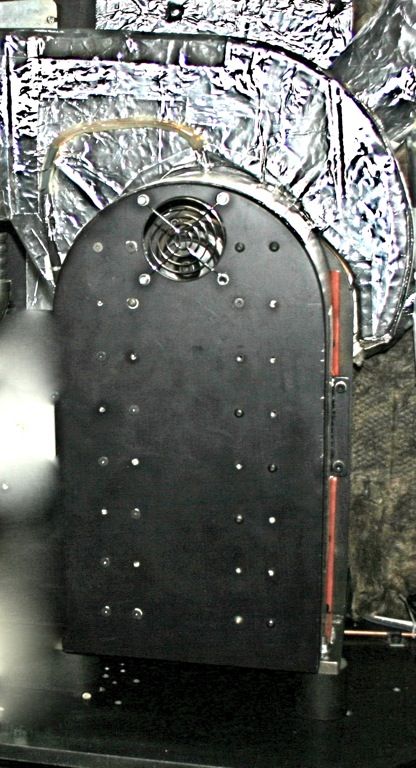
High Temperature Blower II

                                                High Temp. & High Pressure Blower II


Further to the 2012 post "High Temperature Blower at Work"and 2011 post "High Pressure & High Temperature Industrial Blower"; NXT Roasters has been working on an air bearing package that will deliver the same pressure and volume but at higher temperatures.

High temperatures create a hostile environment especially to an object that must turn at high speeds.  Materials must be carefully chosen so that they will maintain their strength and hardness at the elevated temperatures.  Thermal expansion creates problems as well because not only do different materials expand at different rates but various components operate at different temperatures.  That "constant" X 10-6 per °C can really bite you.

Common bearings can handle high temperatures and high speeds but rarely can they do both in the same application.  The high speeds (above 10,000 rpm) mean that the components have to be dynamically balanced plus tight tolerances have to be maintained.

The initial goal was to place the Blower in the coffee roasters where it should easily cope with the 250°C recirculated air.  Curiosity drove the project to higher and higher temperatures.  The current temperature ceiling will remain until a stainless steel housing is fabricated.


Earlier this week a blog reader  requested information on a blower capable of moving flue gases.  Unfortunately the 800°C flue gasses are 300° higher than we have been running the Blower, that temperature is beyond the capacity of the 6061 Blower Housing.  

There are some obvious applications for the Blower but it would be interesting to find out if it is able to solve or enhance some industrial processes.  Email your suggestions and requests to main@nxtroasters.com  .  Perhaps our development plans will coincide.

In the meantime we will continue to accumulate operating hours.


Thursday, 13 December 2012

Coffee Roasting & Heat Transfer

One of the challenges in attempting a discussion that compares roasting environments is that too many "just know that they are right" without doing any tests or measurements.

An untested concept is, more often than not, nonsense.  Transformation processes require laboratory equipment and technical training to understand.  Some technologies have been around for a long time and have been saddled with claims that just do not stand up to scrutiny.  Drum roasting has many devotees that have been critical of other drum roaster users and other roasting methods. There have been several comments of disbelief about the R. Eggers quotation  from  "Espresso Coffee"  in which he claims that "the typical gas temperature of a drum roaster is 400° - 550°C".  The people contesting this did not measure the air temperature in a drum roaster but "felt" that it was way too high.   Now, I have not measured it either but then, I don't have a drum roaster nor do I advocate for their use.  Some drum roasters use heat exchangers which can be fed with variable volumes of air which consequently alters the air temperature sent to the roasting drum.  Perhaps someone will grace us with the range in temperatures achievable and the slope at which changes can be made.   What they don't have is an efficient way of transferring the energy in the air to the beans.   Without a high pressure blower forcing the hot air through the beans it is only possible to transfer significant heat to the outside layer.  In this situation more energy goes up the chimney than into the beans.

Efficient use of energy can only be attained through recirculation of the roasting air which has to be continually scrubbed of smoke to prevent redepositing on the beans.  Untreated air sent to the chimneys is responsible for many chimney fires.

Wednesday, 17 October 2012

High Temperature Blower at Work


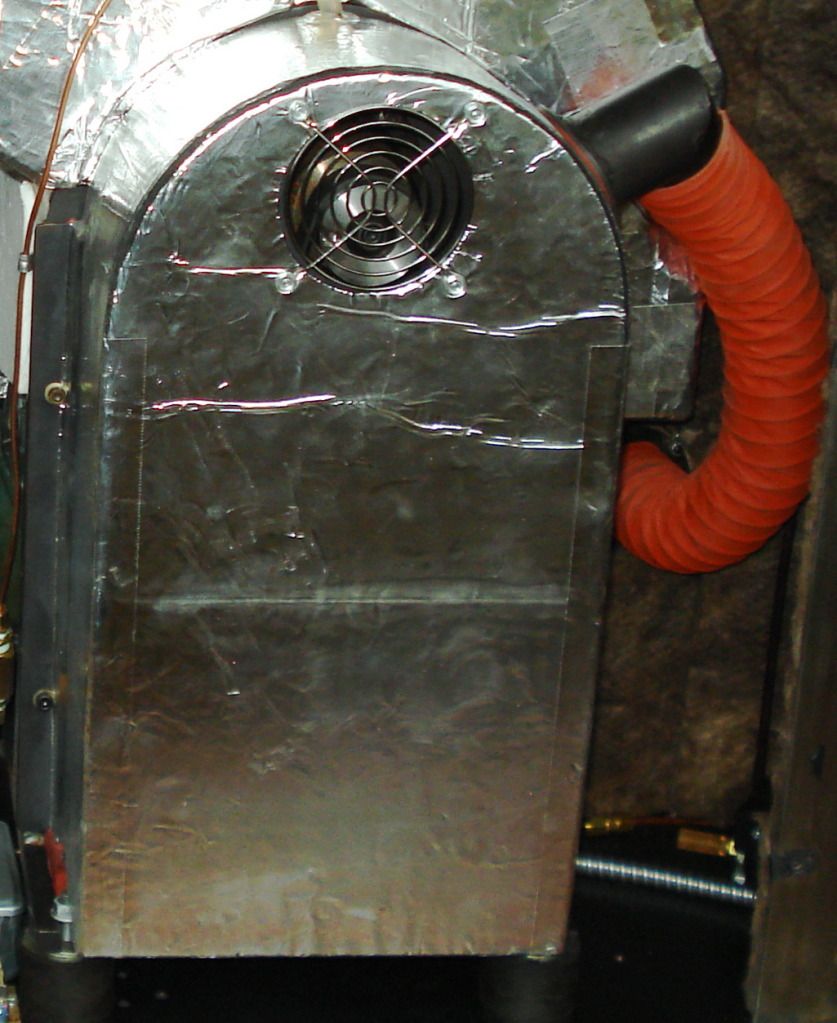
Highly reflective insulation is not an ideal material to photograph but it is easier to blow clean, reflective surfaces do reflect heat, and it effectively contains the ceramic insulation.

The testing has showed that the highest gains in efficiency were made with recirculation of the heated air.  Of course that does create some challenges especially if high pressures are required.  High pressures require positive displacement or high speeds.   Design solutions involve benefit tradeoffs.  A really good design makes use of the component's strengths without being penalized for its shortcomings.

Improving the insulation involves preserving the heated area, facilitating the application of the insulation, and reusing the heat that does escape i.e. air that is used to cool the high speed belt.   To effectively utilize that cooling air there has to be a sufficient temperature differential between it and the item to be heated.  It does work well in preheating a batch because the 70°C flowing air can impart energy to ambient temperature batches.

The air is used to preheat diverse products in order to reduce the load on the main system.  The temperature is too low to create a moisture problem therefore condensation requirements are reserved to the main circuit.  Another efficiency gain would be to use the processed batch to raise the temperature of incoming batch.  Direct contact risks contaminating both batches but heat exchangers have become very efficient providing the throughput is sufficiently high.

Apart from the coffee roasting application we are involved in fluidized bed drying.  A high pressure and high temperature convection oven that can also distribute super heated steam is only in the testing stage.

NOTE: Regarding the comments that this is an old Blower; the Blower is new but the Belt Cover has been repurposed.  The original cover was made from sheet metal only, while this one, had some vibration dampening bars inside.  Further testing showed that noise dampening material was lighter and more effective.  We just kept the old cover for testing prototypes.  Time for a coffee.

Tuesday, 14 August 2012

High Pressure Hot Air Blower - MTBF or Down Time?

High temperatures are not conducive to the longevity of rolling components therefore the conventional ambient blower components have the lifespan of a firefly when used at elevated temperatures.  It is almost a universal mechanical truth that items used at higher temperatures have a reduced working life.  It does not mean that durability is impossible.  It means that durability has to be a priority in the design stage and that components are selected based on their ability at surviving in a high temperature environment.

The focus has been on improving MTBF (mean time before failure) but an alternate viewpoint was raised by a "person in the know".  Essentially the comment was that MTBF is important but "down time" is also a critical factor.  Both of these constitute the inconvenience factor for the client especially if one is low and/or the other is high. 

The insulation required for high temperature equipment does not facilitate repairs therefore the selection of these materials is as important as the blower design itself in facilitating a speedy repair.  With this priority in mind there has been a move towards a faster turn around if a repair or maintenance is required.  The redesign is ongoing and alternative solutions are being tested.

Temperature is but one of the challenges.  We are currently testing blowers that are more tolerant when placed in an environment of "nasty" or corrosive gases.

It is doubtful that the maintenance or repair turn-around will approach Formula 1 tire changing experiences but it promises to be a significant improvement.  It does help to have a crew of 12 to undertake the maintenance if there is sufficient room for everyone to do their task.   It is not likely that such a crew will work unimpeded around a blower therefore it will take longer to affect the change but wages and costs will be lower.

Personally I prefer to take a little longer especially if there is a window of freshly roasted coffee reflection to organize the task.

Cheers,

Sunday, 27 May 2012

High Pressure Hot Air Blower - Sound Containment.

NXT Roasters started with off-the-shelf centrifugal blowers of which we got to know the internals too intimately.  There were no guarantees that they would handle the temperature but the salesperson thought that we should get a reasonable MTBF (Mean Time Before Failure).  At the beginning, it was only 25 hours on average!

Virtually every manufacturer claimed that their composite bearings would work at the 250°C air temperature.  They must not have realized that 18,000 rpm was on the faster side which greatly reduced the life of their product.  Regular bearing races are too soft for this temperature and speed combination.  It takes very little Brinelling which creates a looseness that, at 18K rpm, allows  the shaft to vibrate and the bearings self destruct.  Note: the faster the speed the smaller the movement of the vibration, all other things being equal.  Bearings were repacked with high temperature grease that was measured out in milligrams.  Oil bathed bearings were tried.  Many iterations of new seals had to be turned because the stock items were intended for ambient temperatures. Most modifications succeeded in improving the longevity; 25 hrs, 55 hrs, 125 hrs, 225 hrs, 320 hrs, and after a couple years it was over 1300 hrs.  Not that great, but the client could live with it while we were working on a new blower that is featured in the other blog pages.  A specialized bearing manufacturer made a bearing for us that goes like the proverbial bunny.  All we have to do is pay them a lot of money.  The switch over to our blower design started two years ago.  We do not know the MTBF because of the lack of failures (no! no! that is good).

The aim of this blog is to discuss the blower noise that was generated by that first blower compared to what we have today.

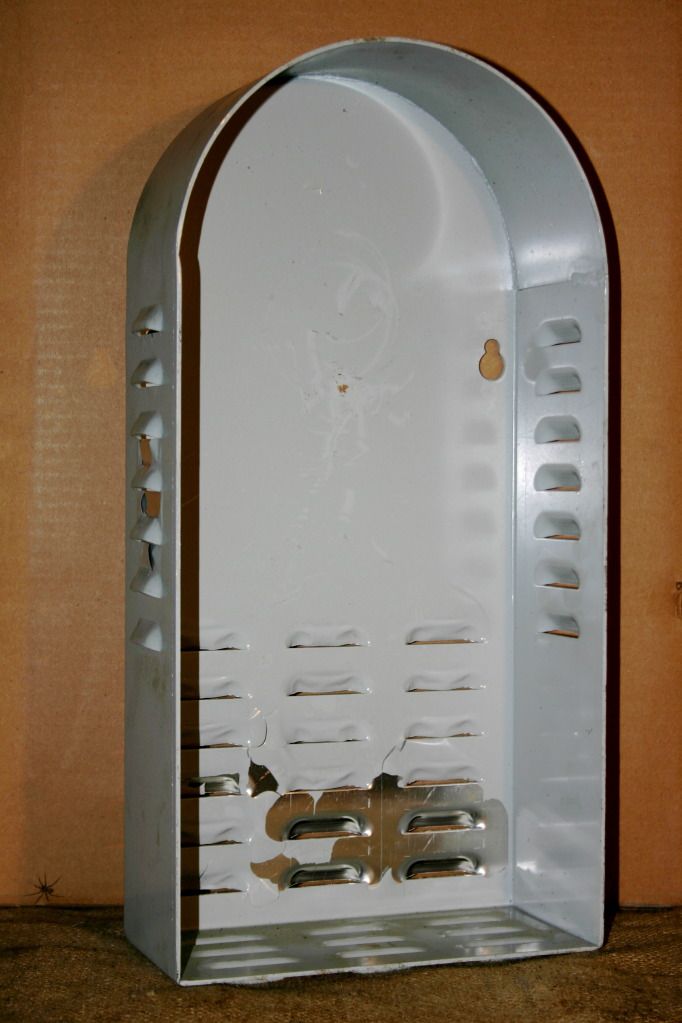
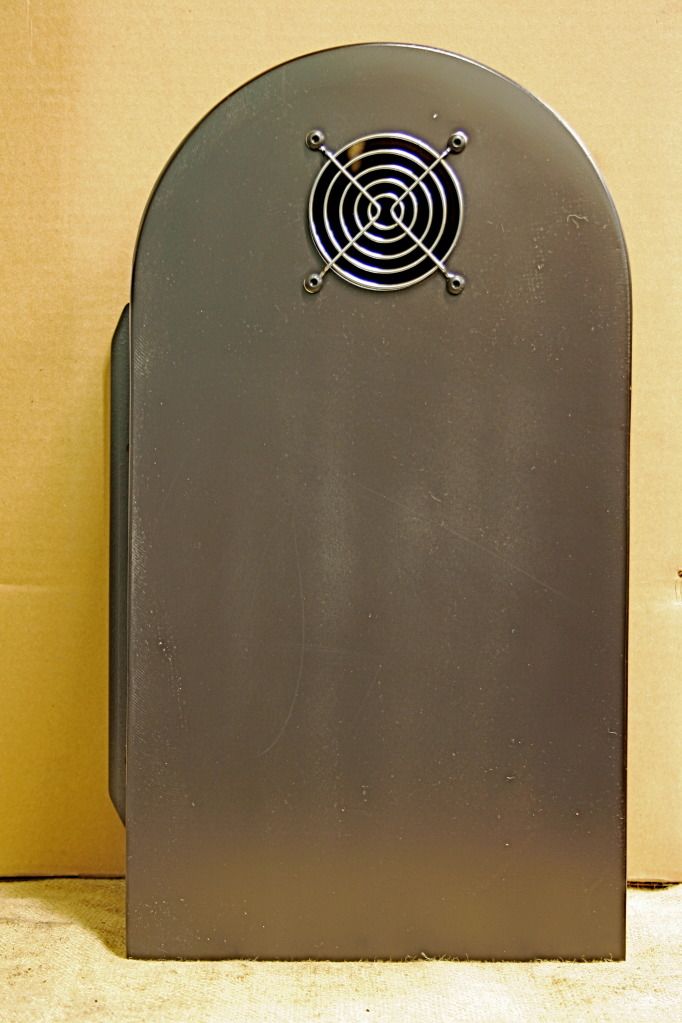
The off the shelf blower had an aluminum Belt Guard with a rubber lip that is not shown.  The guard resonated and the RoastMaster wore Ear Protectors.  Obviously the level of balance is greatly affected by the speed of the 6" Rotor.  If that manufacturer recognizes his cover they will realize that they have a problem and then see the solution.  Well, they have more problems than that which is why they do well to focus on ambient temperatures.  The paint has flaked which reflects badly on the quality of the work.

The output of our design was better than expected therefore we were able to reduce the speed.  To improve upon the case design, first, we increased the mass by making the Belt Guard from steel sheet.  It was better, or as they say, "Good, but not so good".


Heavier bar stock was screwed to the front and sides to increase the mass and reduce the amplitude of the resonance.  The roaster was delivered with that modification but the client still found the noise to be disturbing to the working environment.

In his youth the client was a hot rodder and had some experience with taming unwanted frequencies though I suspect that most of his energy went into making the engine louder.


He covered the Roastaire Belt Guard with an aluminized Butyl Rubber sheet product.  It worked so well that the covering panels got the same treatment.  The "sound treatment" was so effective that CBC Radio did part of "On the Island"  Roastery Interview in front of the working Roastaire.

At the Eptech show Ampco's Rick Gagne discussed such a product that they carry.  It is not necessary to cover much more than 25% of the surface to stop the ringing but esthetics would take a beating with less than full coverage.  The alternative was to place strips on the interior walls but if the bond fails after a while then that will certainly lead to belt failure.   Perhaps we can revisit and find a conclusion after a year - with the help of a freshly roasted coffee.

Wednesday, 16 May 2012

The Importance of Timely Bean Cooling

Coffee is roasted by way of an exothermic reaction.  Without cooling, the beans would invariably burn because they reach the combustion point.   Roasting consistency can only be achieved through the timely introduction of the cooling air, which halts the roasting, to all the beans.

Drum roasting requires well developed skills because there is an extended lag between the moment the RoastMaster views the beans in the Bean Sampler and the termination of the exothermic reaction.  Several factors affect the degree of roast in a drum roaster; the air temperature is considerably higher than what is required for roasting  ("Espresso Coffee" R. Eggers writes the typical gas temperature of a drum roaster is 400° - 550°C. ), using a Bean Sampler is a relatively slow procedure, and the Cooling fans are relatively inefficient at moving air through several layers of beans.  Sucking the air downwards through the beans is also bad design because it packs beans together which greatly hinders air flow.  Many drum roasters spray water on the beans to cool them more quickly.  This is not good nor is it a measured cooling method.

The high temperature cooking analogy for beans hit by the super hot air is cooking Scrambled Eggs while using the stoves highest heat setting.   Even if they are continually mixed the heat is much higher than the egg can transmit to the interior.  The higher heat of the drum roaster still yields a relatively slow roast which highlights the inefficient transfer of energy.         For more details see "" and "Heating Coffee Beans to Roasting Temperature"

It is said that every second counts when "calling the roast" yet it takes many seconds to determine the degree of roast using a Bean Sampler especially if multiple readings have to be taken to follow the progression.

Many roasters are  stressed  by "calling the roast" even after they have been roasting for nine months.  The beans continue to roast during the dumping process and at the beginning of the air cooling cycle.  It is a common drum roasting technique that water is sprayed unto the beans to soak up heat.  It is impossible to accurately meter water coming from a garden hose.  Moisture is the #1 enemy of roasted coffee.  That lingering roast period means the drum RoastMaster must anticipate the roast quite a bit in advance of the required roast level.  An appropriate analogy is shooting ducks; the expert hunter aims for the position where the duck will be when the buckshot arrives.  The hunter must compensate for altitude, shell powder load, temperature, duck speed, and probably many other things that only a good hunter would know. For various reasons a lot of people have a problem with duck hunting (no ducks were harmed for this analogy).  The drum RoastMaster does not deal with less variables.

 To this end the NXT aka Roastaire uses a fluidized bed in which 240°C (adjustable as required) air is pushed, under pressure, through the beans.  This significantly increases the heat transferred to the entire batch of beans.  The beans have a limited ability to absorb the heat therefore the temperature gradient is more uniform throughout the batch with the forced air stream.  The added benefit is that the air flow continually churns the beans and carries away the chaff.

 The beans are cooled within the Roasting Chamber therefore "calling the roast" is done in real time.  The blast of cooling air also churns the beans so that there is even and rapid cooling.  The Roast Monitor communicates to the RoastMaster the roasting progress so that the Cooling Cycle is started at the proper moment.  It only takes a few seconds to cool the beans ( below 180°C according to R.Eggers and below 200°C according to Clarke & Macrae) to stop the roasting process.  After this 30 second Cool Mode the beans are transported to the Packaging Hopper while the NXT aka Roastaire loads nother batch freeing the RoastMaster to appreciate a freshly roasted coffee.

Sunday, 6 May 2012

High Temperature Pressure Gaskets

Several factors have increased the sealing challenges:
- temperature of 250ºC
- a system pressure of 1.1 psi when at roasting temperature
- Hot rolled flanges, not machined surfaces
- it must provide a barrier to very acrid smoke
- must resist suction
- must not out gas after burn in


Silicone sheet was touted to withstand the temperatures but over the years it crystallized and became brittle.  Some Teflons have a fairly high temperature ceiling but most are not nearly as capable and durable as the claims make them out to be.  We attempted to use high temperature ceramic paper but by itself it turned out to be too porous.


Out of curiosity we added a ring of packing material which would further compress the ceramic fibers but it still leaked.

It was possible to seal machined faces with High Temperature paste, some of which was "scaringly" smelly but most of the flanges are cut from hot rolled sheet material.  Better sealing capacity was required over a slightly wavy surface which is exacerbated by the weld to the tubing. 

Samples were cut from various materials that were either on the shelf or purchased.  The initial tests consisted of about four times as many gaskets as shown in the picture above.  A rather simple device was salvaged from the "steel pile" to pressurize the gaskets.  An arbitrary 1.5 atmospheres was selected as the testing pressure.  A soap mixture (sorry I forget the soap's brand-name  which pretty well ruins an endorsement contract) was used to dramatize the results for the camera.  The relative size of the bubbles is proportional to the size of the leak.

We looked for sealing ability especially after being subjected to repeated hot/cool cycles but also the material had to resist extrusion.

Many of the gaskets sealed until they were subjected to periods at 325°C a temperature that was also arbitrarily chosen to represent heat damage over an extended period.  Some people might complain that this is not a fair test.  It might not be but since their product is not named they will not know that they should complain about the procedures.

To the left is a Silicone product that is resistant to 350°C** (you have to search the fine print for the limiting conditions of only being flashed to the temperature on a Wednesday morning between 9:03 and 9:08 AM".  The extruding material created an even greater problem and it was discarded.


To the right is the outside view of the testing oven.  A PID Autonics temperature controller was added with a RTD sensor.  As mentioned above the Set Point is 325°C.  This little throw together may not win an award (it is from the same design studio as the testing jig to the left) but it keeps a stable temperature. 

Seal progress was made through the combination of various products but further work is required to determine the mixture and the method of application so that a uniform gasket is produced.
Personally - I prefer to drink freshly roasted coffee!

Friday, 4 May 2012

High Temperature Blower - Streamlined Inlet

This is another picture of the back of the High Temperature Blower which better shows the Inlet Flange.  In this version the Inlet is attached from inside of the case.   We are currently fabricating an updated version which will be fastened from the outside.

We are working on moulded ceramic insulation but those efforts are not yet worthy of a picture.  To date we have used Cerawool Blanket, ceramic hardboard, and aluminized high temperature fiberglass.  The process is tedious because of the numerous cuts (not all on the insulation) and the challenge to fitting the material to such a "curvy" object.

The unit pictured below has been working 8 hours at 250°C  nearly everyday.  The version, not using the Curved Inlet, is nearly two years old but is used more lightly, though at the same temperature.  A third unit has been used for testing purposes but will soon be used on a nearly daily basis.

A new Inlet Flex Connector has been fabricated and it will soon be tested.  The aim is keep the sound level as low as possible.  We have had a measure of success in accomplishing that.  Last week CBC Radio aired an interview that was done just in front of the working Roastaire.   Obviously more improvements will be implemented to make the work area as pleasant as possible.


Sunday, 22 April 2012

High Pressure Hot Air Blower - Add-ons

We have been reworking the Blower Inlet to improve the air flow and to make the design more compact.  The picture does not show that the Air Inlet has a circular flange but upcoming pictures will better demonstrate those features.

The Air Inlet can be rotated in 45° increments to accommodate various applications.


The Impeller is balanced to better than G.4 standard which is often referred to as gyroscopic level.  The Blower in our application is nevertheless mounted on 2" Rubber Mounts while the Inlet and Outlet are equipped with Flex Pipe to reduce the transmission of vibration from the turning components.  The Flex Pipe photo, above, is the Outlet Connector.  It is rather short due to a constrained space available. Where more space is available a longer Flex Connector can be supplied to add flexibility in the connection to off angle sources or destinations.

Previous attempts to use rolled Flexible Exhaust Pipe resulted in leakage especially at the flange connection.

The Blower output was higher than the expected requirement therefore we were able to reduce the Blower speed to approximately 12,500 rpm.  It is an approximate number due to memory rather than ability to measure accurately.  This modification significantly reduced the background noise generated within the workspace.  The vacuum pulling capacity is still fulfilling the requirements.

Thursday, 15 December 2011

High Pressure & High Temperature Industrial Blower

The suggested applications required either high temperature or high pressure but not both.  Googling the terms "high pressure" "high temperature" Blower brings up every type of air mover imaginable.  The designations are quite "loosey goosey" and often stretched so that it will accommodate the particular product being offered for sale.


I expected that this blower rated at 250°C would be at the bottom end of high temperature blowers but no - some units were given the same designation yet could only operate at temperatures that were 100°C lower.  


Some units had operational ceilings that were twice as high as what this one was tested at but their "high pressure" turned out to be .3 psi or 2,070 pascals which implies that it turns relatively slowly.  Low speeds are attainable with off the shelf bearings.  Therefore, it is not a niche that is of interest.


The version pictured is currently on the test bench where it is subjected to high temperature moist air.  Previous tests of off the shelf blowers demonstrated bearing corrosion in less than 100 hours.  It is possible that had it been a continuous test the bearings would have survived longer but running tests that lasted a few hours compromised the bearings too soon.


We are currently using the blower to fluidize and roast beans (coffee and others).  The pressure output of over 1 psi ( 6,894 pascals ) at 250°C  could certainly fluidize denser materials at a lesser depth.  At these temperatures the blower could be the heart of a monstrous pop corn pumper.  With continual introduction of kernels the output will compete with Vesuvius.  Such a machine would have to be brought to corn country Taber for testing.  


A recycled hot air requirement is fundamental to this niche, otherwise it is more efficient to heat the air after the blower i.e. an air knife.  Now, if a high temperature air knife was in a closed system nearly every blower in the marketplace would be inappropriate.


Hot air accelerated drying in an industrial setting would require a moisture extraction process but if it is a recirculated hot air application this is a custom application.  


Have a freshly roasted coffee and think of another application for the unit.

Thursday, 1 December 2011

High Temperature Industrial Blower

"Delivering the air with sufficient pressure at 240°C is a challenge that will be addressed in a later post.  Sufficient to say that no off the shelf hot air blowers were found, resulting in another product development." from the earlier post Heating Coffee Beans to Roasting Temperature.


Note:  A fan generally turns slower than a blower and therefore cannot reach the same pressure differential (inlet / outlet).  Fluidizing a batch of coffee requires more pressure than a fan delivers.


The easy, but wasteful, way to circulate hot air is to heat it after it passes through the blower.  This means that all the air has to be heated from ambient temperature to final temperature before it is vented while, if the air is recirculated, only the lost heat needs to be replaced.  The higher the temperature the more efficient the recirculation process becomes.  The advantage is not a few percentage points but rather tens of percentage points.


Our prime interest is roasting coffee which becomes much more efficient when the heated air is recirculated.  No off the shelf unit could be purchased.  Initially we tried then modified an existing name brand blower.  The MTBF (mean time before failures) improved from the initial few hours to over 1,500 hours but the maintenance and problems required a new solution.  The concept was simple but mastering the quirks was not always a linear process.


The designed temperature ceiling for the current model is 300°C but it has only been operated up to 270°C.  Since we did not find this to be an optimum roasting temperature the importance of establishing a higher operating threshold lost its urgency.  There is reason to believe that the upper temperature limit can be raised significantly.


Apart from surviving the high temperature the priority is to develop sufficient pressure to create a fluidized bed so that the coffee beans are evenly heated and continually mixed.  The pressure, while roasting, is just under 1 psi (approximately 6 kPa).  This is the flowing pressure not dead head pressure.  


The current blower configuration is driven by a 3 Hp electrical motor connected to a three phase contactor based motor controller.  The Belt Guard Cover was removed for the photo.


Have a freshly roasted coffee and think of another application for the unit.